
This breakdown is written for plant managers, engineers, and operations leaders working in CNC machining, aerospace, automotive, and other precision manufacturing environments where equipment efficiency drives throughput, margin, and on-time delivery. OEE gets referenced constantly on shop floors, yet it's frequently miscalculated or misunderstood once you get past the theory.
Here's what this article covers: the exact formulas behind OEE, a worked example using real numbers, common benchmarks, the mistakes that quietly distort your score, and what to do once you know where you stand.
Key Takeaways
- OEE = Availability × Performance × Quality, showing true productive time within planned production hours
- Discrete manufacturers commonly average 60% OEE, while 85%+ marks top-tier performance
- Accurate OEE depends on consistent, real-time data capture, not end-of-shift guesses or estimates
- Ignoring micro-stops or using an unrealistic cycle time can consistently distort your final OEE number
- Manual tracking works well for single lines, but multi-machine or high-mix shops need automated capture
What Is OEE and Why It Matters in Manufacturing
OEE measures how much of your planned production time results in good parts made at maximum speed. In plain terms, it reveals the gap between what a machine is producing right now and what it could produce running at full capacity, all expressed as one percentage. A score built from machine data alone is incomplete, though: without operator activity, ERP job context and quality inputs, the number tells you something is wrong without telling you why, or what to do about it while the shift is still running.
That single number is what makes OEE useful. Instead of separately tracking downtime logs, cycle-time reports, and scrap rates, you get one figure that reflects all three at once.
OEE differs from two commonly confused metrics:
- Capacity utilization compares actual output to your estimated sustainable capacity, regardless of speed or quality losses.
- Labor productivity measures output per labor hour, which shifts with staffing and scheduling decisions rather than equipment performance.
OEE isolates equipment and process losses specifically. A machine can hit strong OEE during its scheduled runtime while sitting idle most of the week; that's a utilization problem, not an OEE problem.

Where OEE Comes From
OEE originated as a Total Productive Maintenance (TPM) measure, generally credited to Seiichi Nakajima in Japan, and later became a core metric in Lean manufacturing. The Lean Enterprise Institute defines OEE as a TPM measure of how effectively equipment is used, which explains why you'll see it referenced in both TPM and Lean contexts interchangeably.
Despite that Lean pedigree, most shops still fall short of the benchmark. Practitioner sources report that many manufacturers land closer to 60% OEE, with plenty scoring below 45% before they start actively managing losses.
In tight-tolerance industries like CNC machining and aerospace, that gap matters more than usual. Every point of lost Performance or Quality translates directly into scrapped material, missed delivery windows, or rework on parts that were expensive to rough out in the first place.
How to Calculate OEE: Step-by-Step Formula Breakdown
OEE calculation works in two stages: determine Availability, Performance, and Quality separately, then multiply all three together.
Before you start, gather five inputs:
- Planned Production Time - scheduled time minus planned breaks
- Downtime - unplanned stops during that scheduled time
- Ideal Cycle Time - the fastest valid cycle time for the part
- Total Count - all parts produced, good and bad
- Good Count - parts that pass on the first try
Let's walk through a worked example using an 8-hour shift on a CNC mill.
Step 1: Calculate Availability
Formula: Availability = Run Time ÷ Planned Production Time, where Run Time = Planned Production Time − Stop Time
Worked example:
- Shift length: 480 minutes
- Scheduled breaks: 60 minutes → Planned Production Time = 420 minutes
- Unplanned stops (tool changes, alarms, material delays): 47 minutes
- Run Time = 420 − 47 = 373 minutes
- Availability = 373 ÷ 420 = 88.8%
Step 2: Calculate Performance
Formula: Performance = (Ideal Cycle Time × Total Count) ÷ Run Time
Worked example:
- Ideal Cycle Time: 1.0 minute per part
- Total Count during the shift: 300 parts
- Performance = (1.0 × 300) ÷ 373 = 80.4%
That 20% gap represents slower-than-ideal cycles, minor stoppages, and idle time that never showed up as a logged "stop" but still ate into speed.
Step 3: Calculate Quality
Formula: Quality = Good Count ÷ Total Count
Worked example:
- Total Count: 300 parts
- Rejects/rework: 15 parts → Good Count = 285
- Quality = 285 ÷ 300 = 95.0%
Step 4: Multiply the Three Factors for Final OEE
Formula: OEE = Availability × Performance × Quality
Worked example: 0.888 × 0.804 × 0.95 = 0.679, or 67.9% OEE
There's also a simplified single-step formula that produces the identical result, since Run Time and Total Count cancel out algebraically:
OEE = (Good Count × Ideal Cycle Time) ÷ Planned Production Time 285 × 1.0 ÷ 420 = 67.9%
Same answer, fewer steps. OEE.com's calculation guide confirms both formulas as mathematically equivalent, and the shortcut is handy once you already trust your Good Count and cycle time data.

Running these calculations by hand each shift means someone has to track stop times, tally parts, and log rejects manually. Harmoni's real-time OEE monitoring pulls Availability, Performance, and Quality directly from machine data, so this same math runs continuously without anyone tracking it by hand.
What Is a Good OEE Score? Benchmarks and Common Calculation Mistakes
OEE Benchmarks by Performance Tier
Most references treat these tiers as directional, not formal standards:
| Score | What it generally indicates |
|---|---|
| 85%+ | Often cited as world class for discrete manufacturing |
| 60-84% | Fairly typical, with clear room for improvement |
| Below 60% | Significant losses worth investigating |
"Good" depends heavily on your operation. OEE.com notes 85% is "often referred to" as world class, but that figure was built around high-volume, low-mix lines.
A custom aerospace job shop running frequent setups and short batches will naturally see more Availability and startup loss than a line stamping the same part thousands of times a day. Compare your CNC cell against its own trend and part-family history before chasing a generic 85% target.
Common Mistakes That Skew OEE Calculations
Three errors show up again and again on shop floors:
- Inconsistent data collection across shifts. Different stop thresholds and rounding rules make shift-to-shift comparisons meaningless.
- Ignoring micro-stops or rework. Skipping small stoppages in the Performance calculation makes your score look better than reality.
- Using an unrealistic Ideal Cycle Time. A cycle time that's too generous pushes Performance above 100%, a sign the number needs a second look.
Fix: standardize your data dictionary. Define exactly what counts as a stop, what cycle time is "ideal" for each part family, and whether rework counts toward Good Count. Apply it the same way across every shift.
How to Improve OEE Once You Know Your Score
Once you have a number, resist the urge to fix everything at once.
- Identify the biggest loss factor first. Look at Availability, Performance, and Quality separately. If Availability is dragging you down, chasing Performance improvements won't move the needle.
- Run root cause analysis on that one factor. A 5-why exercise on your weakest score usually surfaces two or three fixable causes, rather than a vague list of "everything's a bit off."
- Standardize operator practices and setup procedures. Variability between operators, especially in high-mix CNC environments, quietly drags down both Performance and Quality. A documented setup sheet reduces that variance fast.

Manual vs. Automated Tracking
Spreadsheets and paper logs can work fine for a single line with one operator and a stable part mix. The math is simple enough to do by hand.
The problem shows up as you scale. Multiple machines, multiple shifts, and a rotating mix of jobs mean more data points, more chances for inconsistent logging, and more lag between when a loss happens and when anyone notices it.
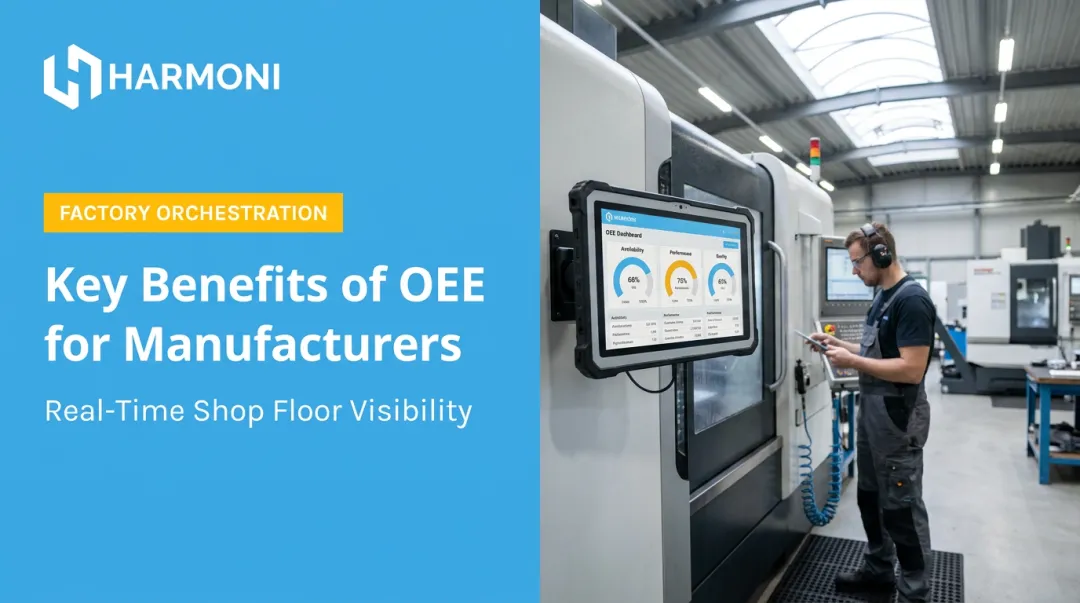
That's the gap Harmoni's factory orchestration platform is built to close. Rather than reconstructing OEE from end-of-shift paper logs, Harmoni connects machine data, operator activity, and ERP workflows in real time, so Availability, Performance, and Quality inputs update as production happens, not after the fact.
That real-time visibility catches losses while they're still fixable. It also feeds into more accurate job costing, since the actual cycle times and labor records driving your OEE score are the same ones driving your cost data.
Conclusion
OEE quantifies how much of your planned production time is truly productive by combining Availability, Performance, and Quality into one score. The formulas aren't complicated. Applying them consistently, shift after shift, is where most operations fall short.
Repeatable data collection beats one-time precision every time. A perfectly calculated OEE from a single shift tells you less than a rough number tracked consistently for a month. Real-time visibility into the inputs behind OEE turns the score from a lagging report into something you can act on while production is still running. Harmoni's factory orchestration platform builds that visibility in automatically, pulling machine, operator, and ERP data into one live view so shop floor teams can catch problems before a shift ends, not after the numbers come in.
Frequently Asked Questions
How to calculate Overall Equipment Effectiveness?
Multiply Availability, Performance, and Quality (each as a percentage) to get OEE. See the step-by-step breakdown above for the exact formulas and a worked example using an 8-hour shift.
What is a good OEE score?
85%+ is considered world class for discrete manufacturing, 60-84% is typical with room to improve, and below 60% signals significant losses worth investigating.
How often should OEE be measured?
Calculate it per shift and review daily to spot trends before they become bigger problems. Longer-term aggregation is useful for reporting, but daily review catches issues while they're still fixable.
Is OEE the same as productivity?
No. Productivity typically includes labor and planning factors, while OEE isolates equipment and process performance, covering downtime, speed loss, and defects.
What data do you need to calculate OEE accurately?
You need Planned Production Time, downtime, Ideal Cycle Time, Total Count, and Good Count. Missing or inconsistent data in any of these five inputs will distort your final score.
How does OEE fit into Lean manufacturing and TPM?
OEE originated within Total Productive Maintenance and quantifies process waste, downtime, speed loss, and defects, giving Lean teams a measurable baseline for continuous improvement efforts.