November 4, 2026
Building the Factory of the Future Starts with the Factories We Have
Read More
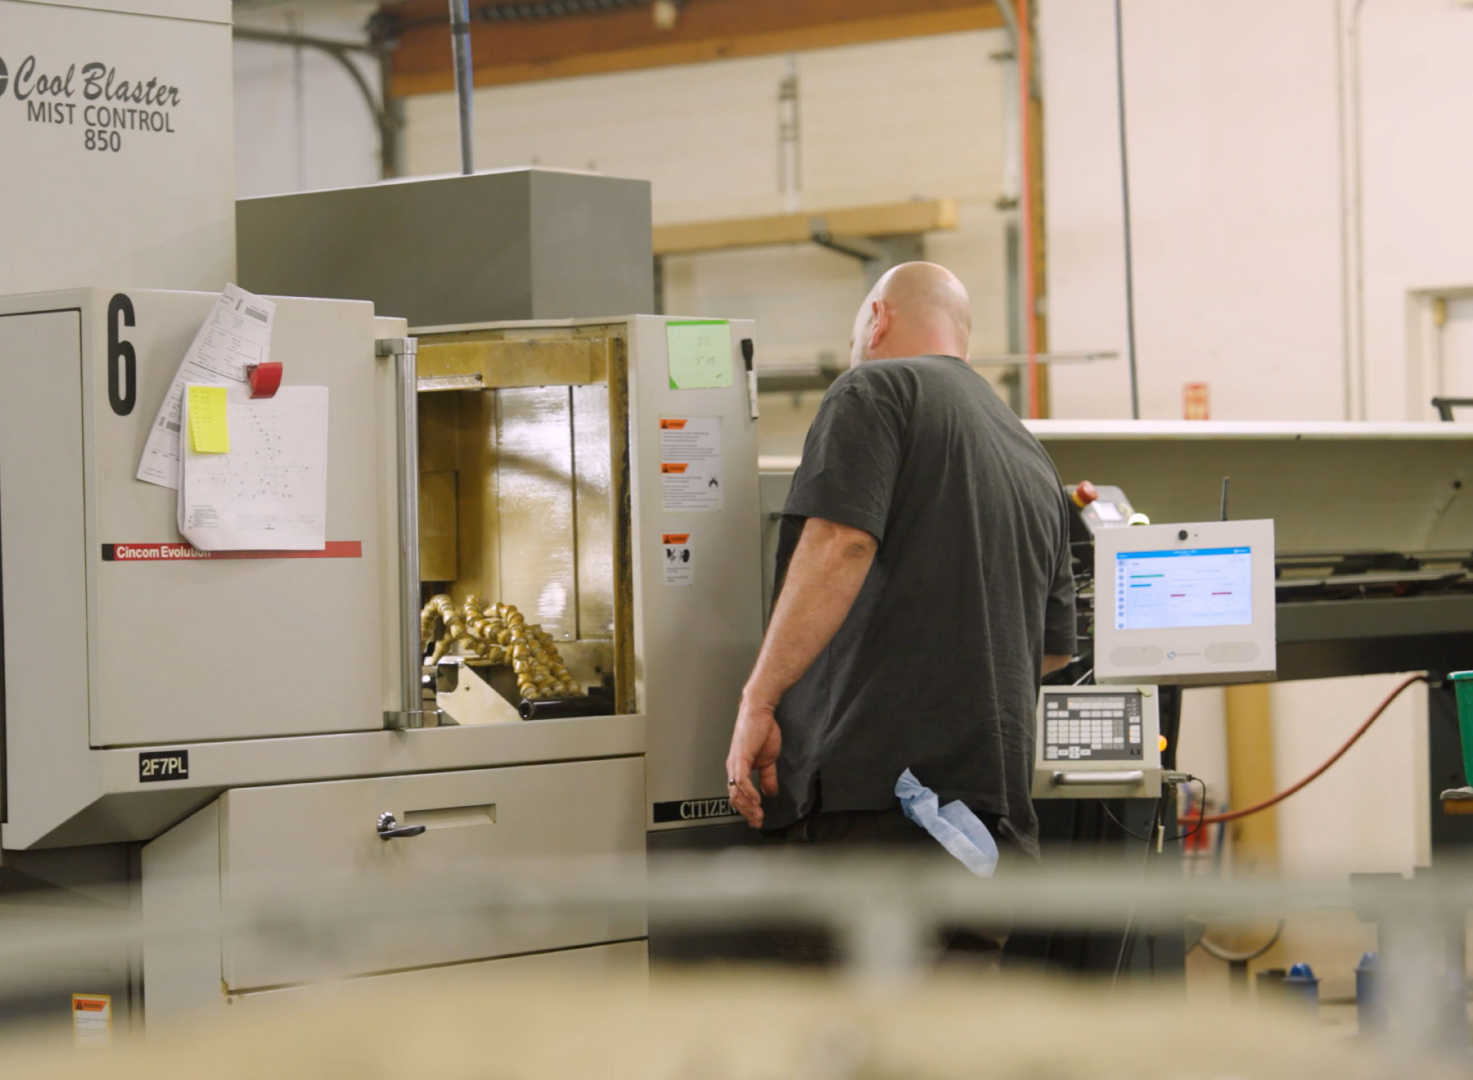
When orders are stacking up, buying another machine can seem like the clearest way to add capacity. But a growing backlog does not always mean the factory has run out of machine capacity. Work may be concentrated at one operation, production estimates may not reflect actual conditions, or available hours may be lost to setup, waiting, maintenance, or scheduling constraints.
Before committing to new equipment, manufacturers need a reliable picture of how existing capacity is being used—and where work is actually getting stuck. Machine utilization and OEE can help, but neither metric answers the investment question on its own. They become more useful when reviewed alongside job requirements, backlog, shift schedules, and production flow.
Machine utilization compares the time a machine is producing with the time it was available or scheduled to run. It can help identify equipment that is frequently idle, heavily loaded, or used differently than expected.
The definition matters. A machine that runs for 70% of scheduled time may be performing well if the remaining time is planned for changeovers, maintenance, or low demand. The same figure may point to a problem if jobs are waiting, operators cannot get support, or unplanned downtime is high. Utilization should be interpreted against the schedule and the work the machine is expected to perform.
OEE, or overall equipment effectiveness, looks at availability, performance, and quality together. It can help teams examine losses while equipment is scheduled to produce. Like any summary measure, OEE is most useful when teams can also see the underlying events and agree on how each factor is calculated.
A plant-wide average can hide important differences between machine groups, shifts, and types of work. One machine may have available hours while another machine on the critical route is consistently overloaded. A machine may appear underused because its work arrives in batches, because it is waiting on inspection, or because the schedule does not reflect actual routing.
OEE is also not a direct measure of total factory capacity. It describes performance during defined production time. It does not tell a manufacturer whether customer demand will continue, whether jobs can move to another workcenter, or whether a new machine would relieve the actual constraint.
For capacity planning, the useful question is not simply “What is our OEE?” It is “Which operations are limiting the work we need to complete, and why?”
Start with the jobs that are late, at risk, or driving the backlog. Map their routings and identify which operations are common to those jobs. Look for recurring queues and wait times, not just machines with high utilization.
The constraint may be a particular machine group, but it could also be programming, setup, inspection, material availability, or access to skilled labor. Adding equipment helps only when the new resource addresses the limiting step.
Estimate the machine hours needed to complete current and planned work. Use actual job history where possible, and account for setup, changeovers, maintenance, scheduled downtime, and the mix of jobs expected. Compare that requirement with realistic staffed hours—not the theoretical maximum hours in a calendar.
If estimates consistently differ from actual run times, review how routings and standards are created. Capacity calculations based on inaccurate assumptions can make a plant look short of equipment when the issue is its planning data.
Separate the data enough to see patterns. Averages across the whole plant can mask overloaded workcenters or underused shifts. Compare similar machines and similar jobs where possible, and look at how performance changes with setup complexity, lot size, or operator availability.
This helps answer practical questions: Is one workcenter carrying most of the load? Is a particular shift constrained? Are certain jobs routinely taking longer than planned? Are machines waiting for work, or is work waiting for machines?
When a machine is idle or running below its expected rate, find out what was happening. Was it waiting for material, a program, a setup, an inspection, maintenance, or a decision? Was the job estimate unrealistic? Is the machine not suited to the current mix?
Machine status and OEE can highlight where to investigate. Job and production context help explain the cause. Record downtime categories consistently and keep the list practical; overly broad or overly detailed reason codes can make the data harder to interpret.
Once the constraint is clearer, compare options. Depending on the situation, a manufacturer might rebalance work across compatible machines, adjust shift coverage, improve setup processes, revise scheduling rules, address a recurring maintenance issue, or invest in new equipment.
Estimate the effect of each option on throughput, lead times, labor, quality, and operating cost. A new machine may be the right decision, but the analysis should show which jobs it will support and how it changes the limiting step. If another process becomes the constraint immediately, the expected capacity gain may not materialize.
A useful capacity review looks at a small group of connected measures rather than a single score:
Review these measures over a period that reflects the plant’s production cycle. A short window may be distorted by an unusual job or planned maintenance; a long average may hide a recent change in demand or performance. The right timeframe depends on the operation and how often its work mix changes.
Machine utilization and OEE are useful inputs to manufacturing capacity planning, but they are not verdicts. They help show where to investigate. Backlog, routings, labor availability, job history, and the causes of lost time help determine what action is likely to relieve the constraint.
For manufacturers, shop floor visibility means being able to understand how machine activity relates to the work being performed. When that context is available, operations and finance teams can evaluate equipment proposals against the actual production need—and revisit the decision as demand and the job mix change.
Factory Orchestration is one approach to bringing machine activity, production work, and process information into a more connected operational view. The practical objective is straightforward: make capacity decisions using a clearer picture of how work moves through the factory.